What is the High Barrier Packaging Films for Pharmaceuticals Market Size and Growth Rate?
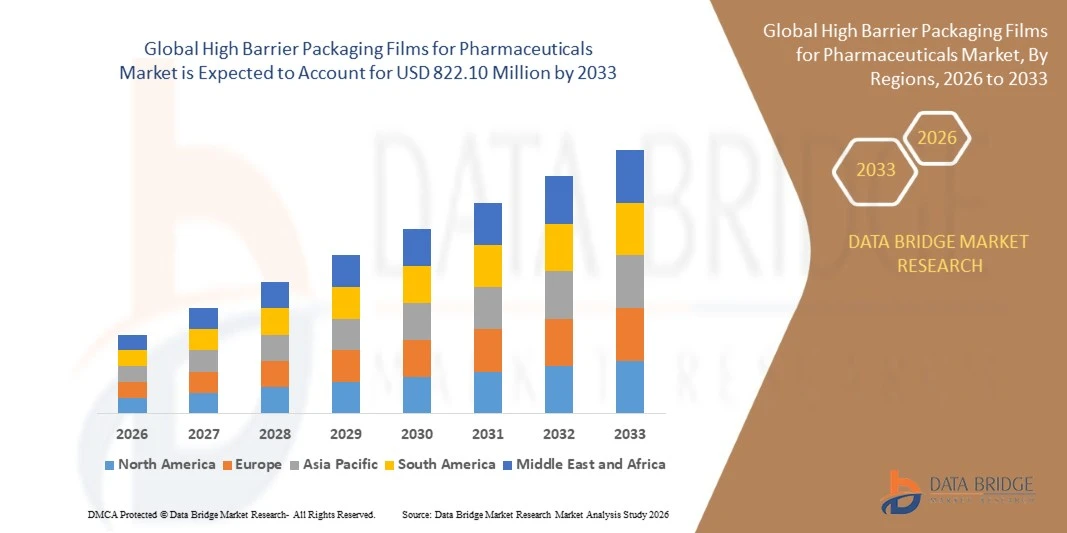
- As per Data Bridge Market Research analysis, the high barrier packaging films for pharmaceuticals market was valued at USD 519.71 million in 2025 and is projected to reach USD 822.10 million by 2033, growing at a CAGR of 5.90% from 2026 to 2033.
- The market is experiencing consistent growth driven by rising demand for enhanced pharmaceutical product protection, increasing adoption of advanced flexible packaging materials, and expanding applications across pharmaceutical manufacturing, drug delivery, and healthcare packaging.
- The increasing demand for extended shelf life and protection against moisture, oxygen, light, and other external contaminants, combined with stringent pharmaceutical packaging regulations, is compelling drug manufacturers to adopt high barrier packaging films. Advanced multilayer films and high-performance polymer materials are increasingly being used in blister packs, pouches, and sachets, offering improved product stability, contamination prevention, and reliable packaging solutions for sensitive pharmaceutical products.
Market Size & Forecast
- Global Market Value (2025): USD 519.71 Million
- Expected Market Value (2033): USD 822.10 Million
- Forecast CAGR (2026–2033): 5.90%
- Leading Region in 2025: North America
- Fastest Growing Region: Asia Pacific
What are the Major Takeaways of the High Barrier Packaging Films for Pharmaceuticals Market?
- North America dominated the high barrier packaging films for pharmaceuticals market with the largest revenue share of 35.4% in 2025, supported by advanced pharmaceutical manufacturing infrastructure, stringent regulatory standards, and rising demand for high-performance drug packaging materials.
- Asia-Pacific is expected to be the fastest-growing region at a CAGR of 7.2% from 2026 to 2033, fueled by expanding pharmaceutical production, rising healthcare expenditure, and increasing investments in advanced packaging technologies across China, India, and Japan.
- The metalized films segment led the market with a 38.5% share in 2025, driven by its excellent barrier properties against moisture, oxygen, and light.
- Inorganic oxide coating films are the fastest-growing type, projected to register a CAGR of 7.2%, reflecting the surge in demand for transparent packaging with high oxygen and moisture barrier performance.
- The cold-formable films segment dominated the product category with a 42.5% revenue share in 2025, led by its widespread use in pharmaceutical blister packaging.
- Aluminum accounted for 54.0% of the market share in 2025, preferred by its excellent barrier protection against moisture, oxygen, light, and external contaminants.
- The sustainable barrier coating segment is the fastest-growing technology category, with a CAGR of 7.5%, driven by increasing demand for pharmaceutical packaging that combines product protection with improved environmental performance.
Report Scope and High Barrier Packaging Films for Pharmaceuticals Market Segmentation
|
Attributes |
High Barrier Packaging Films for Pharmaceuticals Key Market Insights |
|
Segments Covered |
|
|
Countries Covered |
North America
Europe
Asia-Pacific
Middle East and Africa
South America
|
|
Key Market Players |
|
|
Market Opportunities |
|
|
Value Added Data Infosets |
In addition to the insights on market scenarios such as market value, growth rate, segmentation, geographical coverage, and major players, the market reports curated by the Data Bridge Market Research also include import export analysis, production capacity overview, production consumption analysis, price trend analysis, climate change scenario, supply chain analysis, value chain analysis, raw material/consumables overview, vendor selection criteria, PESTLE Analysis, Porter Analysis, and regulatory framework. |
What is the Key Trend in the High Barrier Packaging Films for Pharmaceuticals Market?
- Pharmaceutical manufacturers are increasingly adopting high barrier packaging films to protect sensitive medicines from moisture, oxygen, light, and external contamination while extending product shelf life.
- For instance, in June 2025, Honeywell announced that Evertis selected its Aclar film technology for its Evercare pharmaceutical brand to improve moisture-barrier protection, support drug stability, and develop recyclable PET-based pharmaceutical packaging materials.
- Multilayer polymer structures and specialized barrier coatings enable packaging manufacturers to enhance product stability while maintaining the flexibility and durability required for pharmaceutical applications.
- Pharmaceutical companies are increasingly exploring recyclable high barrier packaging materials to reduce environmental impact without compromising the protective performance required for sensitive drug formulations.
- For instance, in October 2024, Bayer and Liveo Research launched PET blister packaging for Aleve, eliminating PVC and reducing the packaging's carbon footprint by 38% compared with the previous packaging, reflecting the shift toward more sustainable pharmaceutical packaging materials.
- As pharmaceutical manufacturers prioritize drug stability, packaging sustainability, and regulatory compliance, demand for advanced barrier films is expected to increase, reinforcing their importance in modern pharmaceutical packaging.
What are the Key Drivers of the High Barrier Packaging Films for Pharmaceuticals Market?
- The growing production of biologics, injectable medicines, and moisture-sensitive drugs is increasing demand for high barrier packaging films that maintain product stability and protect pharmaceutical formulations throughout storage and distribution.
- For instance, in June 2024, TekniPlex Healthcare developed coextruded multilayer barrier film solutions for sterile liquid drug reservoirs, addressing the need to maintain drug stability for up to two years while minimizing moisture loss and protecting against interactions with pharmaceutical ingredients
- Pharmaceutical manufacturers are integrating advanced multilayer films and specialized polymer coatings into packaging operations to improve barrier performance, reduce product degradation, and meet increasingly demanding drug protection requirements
- For instance, in January 2024, TekniPlex Healthcare partnered with Alpek Polyester to introduce a pharmaceutical-grade PET blister film containing 30% post-consumer recycled content, designed to maintain pharmaceutical quality standards while supporting recyclable packaging solutions.
- As pharmaceutical production expands and drug formulations become more sensitive to environmental conditions, high barrier packaging films will remain essential for maintaining product quality, supporting longer shelf life, and ensuring reliable drug delivery.
What Factors are Challenging the Growth of the High Barrier Packaging Films for Pharmaceuticals Market?
- High barrier pharmaceutical packaging films require specialized polymers, multilayer structures, advanced coating technologies, and precision manufacturing processes, increasing production costs compared with conventional packaging materials.
- For instance, in July 2025, LOG Pharma Primary Packaging reported that a pharmaceutical manufacturer faced repeated stability failures with a moisture-sensitive and oxygen-sensitive tablet using conventional HDPE bottles, despite using desiccants and oxygen scavengers. The case highlights the added material costs and packaging complexity involved in protecting sensitive drug formulations.
- These elevated material and processing costs can limit adoption among smaller pharmaceutical manufacturers, particularly when packaging solutions require specialized equipment, regulatory validation, and compatibility testing.
- The complexity of pharmaceutical packaging qualification, combined with recycling challenges associated with certain multilayer film structures, continues to create technical and financial barriers for manufacturers seeking cost-effective, compliant, and sustainable packaging solutions.
- For instance, in April 2025, an article published in Macromolecular Materials and Engineering highlighted that multilayer polymer barrier films are difficult to recycle because of their complex material compositions and strong interlayer adhesion, creating technical challenges for pharmaceutical packaging manufacturers seeking sustainable alternatives.
- These production costs, material compatibility requirements, and stringent performance validation procedures can slow the adoption of advanced barrier films, particularly among price-sensitive manufacturers, despite growing demand for reliable pharmaceutical packaging.
How is the High Barrier Packaging Films for Pharmaceuticals Market Segmented?
The high barrier packaging films for pharmaceuticals market is segmented on the basis of type, product, material, technology, and application.
- By Type
On the basis of type, the high barrier packaging films for pharmaceuticals market is segmented into metalized films, clear films, organic coating films, and inorganic oxide coating films. The metalized films segment dominated the market with an estimated 38.5% share in 2025, owing to its excellent barrier properties against moisture, oxygen, and light. These films use a thin metallic layer, commonly aluminum, to enhance protection for sensitive pharmaceutical formulations. They are widely used in blister packaging, sachets, and flexible pharmaceutical packs requiring extended shelf life. Their ability to reduce exposure to external environmental conditions supports product stability during storage and distribution. Cost-effective barrier performance and compatibility with multilayer packaging structures further strengthen adoption.
The inorganic oxide coating films segment is projected to register the fastest growth at an estimated CAGR of 7.2% from 2026 to 2033, driven by increasing demand for transparent packaging with high oxygen and moisture barrier performance. These films typically incorporate thin layers of silicon oxide or aluminum oxide on polymer substrates. They allow pharmaceutical manufacturers to maintain product visibility while providing protection against environmental degradation. Their suitability for lightweight flexible packaging supports applications involving sensitive drugs and specialized formulations. Improvements in coating uniformity, flexibility, and manufacturing efficiency are expanding their potential applications.
- By Product
On the basis of product, the high barrier packaging films for pharmaceuticals market is segmented into cold-formable films, coextruded films, and thermo-formable films. The cold-formable films segment dominated the market with an estimated 42.5% share in 2025, supported by its widespread use in pharmaceutical blister packaging. These films can be shaped without conventional heat-forming processes, allowing packaging to achieve strong protection against moisture, oxygen, and light. Aluminum-based cold-forming structures are particularly suitable for sensitive medicines that require strong environmental barriers. Their ability to provide individual cavity protection helps preserve product integrity and minimize exposure during storage. They are widely used for tablets, capsules, and other solid dosage forms.
The coextruded films segment is projected to register the fastest growth at an estimated CAGR of 7.0% from 2026 to 2033, driven by demand for integrated barrier properties within a single manufactured film structure. Coextrusion combines multiple polymer layers to deliver different functions, including sealing, mechanical strength, and resistance to moisture or oxygen. This approach can reduce the need for separate lamination steps and support efficient packaging production. Manufacturers can tailor layer composition to meet specific pharmaceutical protection requirements. Advances in polymer technology are enabling thinner structures with improved performance and material efficiency. Rising demand for flexible pharmaceutical packaging and customized barrier solutions is expected to encourage further adoption.
- By Material
On the basis of material, the high barrier packaging films for pharmaceuticals market is segmented into aluminum and plastics. The aluminum segment dominated the market with an estimated 54.0% share in 2025, owing to its excellent barrier protection against moisture, oxygen, light, and external contaminants. Aluminum is widely used in pharmaceutical blister packs, foil laminates, sachets, and specialized packaging structures. Its near-total barrier performance makes it suitable for sensitive medicines requiring extended stability and reliable protection. The material also supports tamper-evident and unit-dose packaging applications. Increasing demand for pharmaceutical products with stringent shelf-life requirements is supporting its adoption.
The plastics segment is projected to register the fastest growth at an estimated CAGR of 6.8% from 2026 to 2033, driven by increasing demand for lightweight, flexible, and versatile pharmaceutical packaging materials. Polymers such as polyethylene, polypropylene, polyethylene terephthalate, and polyamide are used in multilayer films and specialized barrier structures. These materials provide flexibility, sealability, mechanical strength, and compatibility with different packaging formats. Advances in polymer blends, multilayer coextrusion, and high-performance coatings are improving their moisture and oxygen barrier properties. Plastic-based films can also support transparent packaging, allowing visual inspection of pharmaceutical products. Growing interest in recyclable structures and material-efficient packaging is expected to further encourage innovation in this segment.
- By Technology
On the basis of technology, the high barrier packaging films for pharmaceuticals market is segmented into multilayer film, sustainable barrier coatings, Besela barrier film, and others. The multilayer film segment dominated the market with an estimated 47.5% share in 2025, owing to its ability to combine different materials to achieve enhanced barrier performance. These structures can integrate moisture resistance, oxygen protection, heat sealability, and mechanical durability within a single packaging system. They are widely used in pharmaceutical blister packs, pouches, sachets, and laminated packaging. Manufacturers can customize the composition and thickness of individual layers according to the sensitivity of the packaged drug. Multilayer films also support compatibility with high-speed packaging equipment and different pharmaceutical dosage forms.
The sustainable barrier coatings segment is projected to register the fastest growth at an estimated CAGR of 7.5% from 2026 to 2033, driven by increasing demand for pharmaceutical packaging that combines product protection with improved environmental performance. These coatings can enhance the barrier properties of paper-based and polymer-based substrates without relying entirely on conventional multilayer structures. Advances in water-based coatings, thin-film technologies, and recyclable coating formulations are expanding their application potential. Pharmaceutical packaging manufacturers are exploring these solutions to reduce material consumption and improve packaging recyclability. Maintaining consistent barrier performance, chemical compatibility, and regulatory compliance remains essential for pharmaceutical applications. Continued innovation in sustainable coating technologies is expected to support adoption as manufacturers seek to balance drug protection with environmental considerations.
- By Application
On the basis of application, the high barrier packaging films for pharmaceuticals market is segmented into pouches, bags, lids, shrink films, laminated tubes, and others. The pouches segment dominated the market with an estimated 32.5% share in 2025, driven by the widespread use of flexible packaging for pharmaceutical products and medical preparations. High barrier pouches can protect their contents from moisture, oxygen, light, and external contamination, depending on the material structure. They are used for powders, granules, medical components, and selected pharmaceutical formulations. Their lightweight construction helps reduce transportation and storage requirements compared with some rigid packaging alternatives. Pouches can incorporate multilayer films, specialized coatings, and heat-sealable layers to meet specific product protection requirements.
The laminated tubes segment is projected to register the fastest growth at an estimated CAGR of 6.9% from 2026 to 2033, supported by demand for protective packaging for pharmaceutical creams, gels, ointments, and topical formulations. Laminated tubes combine polymer layers and barrier materials to protect formulations against environmental exposure and preserve product quality. Their structure can provide controlled dispensing, convenient handling, and protection against contamination during repeated use. High barrier laminates are particularly useful for formulations that are sensitive to oxygen, moisture, or external contaminants. Improvements in tube sealing, material compatibility, and recyclable laminate development are expanding packaging options for pharmaceutical manufacturers. Increasing demand for topical medicines and convenient dispensing formats is expected to support further growth.
Which Region Holds the Largest Share of the High Barrier Packaging Films for Pharmaceuticals Market?
- North America dominated the high barrier packaging films for pharmaceuticals market with the largest revenue share of 35.4% in 2025, supported by advanced pharmaceutical manufacturing infrastructure, stringent regulatory standards, and rising demand for high-performance drug packaging materials.
- The region also benefits from established pharmaceutical supply chains, substantial investment in drug development, and increasing demand for packaging solutions that protect sensitive medicines against moisture, oxygen, and light. The presence of leading packaging manufacturers and growing adoption of advanced barrier technologies continue to strengthen North America's position in the global market.
U.S. High Barrier Packaging Films for Pharmaceuticals Market Insight
The U.S. high barrier packaging films for pharmaceuticals market is witnessing steady growth due to rising demand for advanced pharmaceutical packaging solutions, increasing production of sensitive medicines, and growing emphasis on drug safety and shelf-life extension. The country’s established pharmaceutical manufacturing ecosystem, along with increasing adoption of multilayer films, specialized polymer materials, and advanced barrier coatings, is driving demand across pharmaceutical packaging applications. In addition, stringent quality standards and the need to protect medicines from moisture, oxygen, light, and contamination are accelerating the adoption of high barrier packaging films.
Asia-Pacific High Barrier Packaging Films for Pharmaceuticals Market Insight
The Asia-Pacific high barrier packaging films for pharmaceuticals market is expected to witness rapid growth, driven by expanding pharmaceutical manufacturing, increasing healthcare expenditure, and rising demand for reliable drug packaging solutions across countries such as China, India, and Japan. Growing production of generic medicines, increasing investments in pharmaceutical infrastructure, and rising awareness regarding drug stability are supporting regional market expansion. In addition, the growing adoption of advanced multilayer packaging technologies and sustainable barrier materials is accelerating demand across pharmaceutical manufacturers and packaging suppliers.
Japan High Barrier Packaging Films for Pharmaceuticals Market Insight
The Japan high barrier packaging films for pharmaceuticals market is witnessing consistent growth due to rising demand for high-quality pharmaceutical packaging, increasing production of sensitive medicines, and a strong focus on drug safety and product stability. Pharmaceutical manufacturers are increasingly adopting advanced barrier films and specialized coating technologies to protect medicines from moisture, oxygen, light, and external contamination. Moreover, growing emphasis on packaging quality, material innovation, and sustainable pharmaceutical packaging solutions is further contributing to market growth.
China High Barrier Packaging Films for Pharmaceuticals Market Insight
The China high barrier packaging films for pharmaceuticals market is growing rapidly, driven by expanding pharmaceutical production, rising healthcare demand, and increasing investments in advanced packaging technologies. Growing adoption of multilayer films, coextruded structures, and high-performance barrier coatings across pharmaceutical applications is significantly boosting market demand. In addition, increasing focus on drug quality, longer shelf life, packaging innovation, and the development of domestic pharmaceutical manufacturing capabilities is positioning China as an important growth market for high barrier packaging films.
U.K. High Barrier Packaging Films for Pharmaceuticals Market Insight
The U.K. high barrier packaging films for pharmaceuticals market is experiencing steady growth, supported by rising demand for protective pharmaceutical packaging, increasing emphasis on medicine stability, and continued innovation in packaging materials. Growing investments in advanced film structures and barrier coating technologies are contributing to market growth across pharmaceutical manufacturing and packaging applications. Furthermore, increasing focus on recyclable packaging materials, regulatory compliance, and protection against moisture, oxygen, and light is encouraging the adoption of high barrier films across the U.K. pharmaceutical industry.
Germany High Barrier Packaging Films for Pharmaceuticals Market Insight
The Germany high barrier packaging films for pharmaceuticals market is expanding steadily due to the country’s strong pharmaceutical manufacturing base, advanced packaging capabilities, and increasing adoption of innovative barrier materials. Pharmaceutical companies and packaging manufacturers are increasingly utilizing multilayer films, specialized polymers, and advanced coatings to improve drug protection, shelf life, and packaging performance. Continuous advancements in sustainable packaging structures, material efficiency, and barrier technology, along with a strong focus on pharmaceutical quality and regulatory compliance, are further driving market growth in Germany.
Which are the Top Companies in High Barrier Packaging Films for Pharmaceuticals Market?
The high barrier packaging films for pharmaceuticals industry is primarily led by well-established companies, including:
- ACG Pharmapack Pvt. Ltd. (India)
- Amcor plc (Switzerland)
- Constantia Flexibles Group GmbH (Austria)
- Klöckner Pentaplast (Germany)
- Perlen Packaging AG (Switzerland)
- Liveo Research GmbH (Germany)
- Tekni-Plex, Inc. (U.S.)
- Honeywell International Inc. (U.S.)
- Bilcare Limited (India)
- Huhtamaki Oyj (Finland)
- SÜDPACK Verpackungen SE & Co. KG (Germany)
- UFlex Limited (India)
- Jindal Films (India)
- Toray Industries, Inc. (Japan)
- Mitsubishi Chemical Group Corporation (Japan)
- Sumitomo Bakelite Co., Ltd. (Japan)
- HySum Europe GmbH (Germany)
- Winpak Ltd. (Canada)
- Evertis Europe, S.A. (Portugal)
- Dai Nippon Printing Co., Ltd. (Japan)
What are Latest Developments in High Barrier Packaging Films for Pharmaceuticals Market?
- In July 2025, Dai Nippon Printing (DNP) announced the development of a vacuum-metallized high-barrier polypropylene (PP) film designed to provide oxygen, water-vapor, and light protection. The company stated that its barrier performance was nearly twice that of its conventional mono-material packaging. The film is intended for packaging applications including medicines and can support mono-material structures designed to improve recyclability.
- In June 2025, Honeywell announced that Evertis had selected its Aclar barrier film technology for its Evercare pharmaceutical packaging brand. The collaboration is intended to support medical-grade PET packaging with strong moisture-barrier properties, helping protect drug stability and extend shelf life. The companies also highlighted thermoforming, sealing, optical performance, and improved recyclability as important features of the planned packaging materials.
- In January 2024, TekniPlex Healthcare and Alpek Polyester introduced a pharmaceutical-grade PET blister film containing 30% post-consumer recycled content using Alpek’s Octal rDPET technology. The film was designed for pharmaceutical primary packaging and can be combined with compatible polyester lidding to create a recyclable blister system where appropriate recycling infrastructure exists. This launch demonstrated efforts to incorporate recycled content into pharmaceutical barrier packaging while retaining essential packaging functionality.
- In October 2023, Solvay launched Diofan® Ultra736, a high-performance polyvinylidene chloride (PVDC) coating solution developed for pharmaceutical blister films. The coating was designed to provide strong water-vapor barrier performance while retaining oxygen-barrier properties, transparency, and thermoformability. It also allows thinner coating structures, potentially reducing material use and the environmental footprint of pharmaceutical blister packaging.
- In April 2022, Huhtamaki launched Push Tab, an aluminum-free, mono-material PET blister-lidding solution developed with Klöckner Pentaplast for the pharmaceutical and healthcare industries. The product was designed to improve packaging recyclability while meeting pharmaceutical packaging safety requirements and operating on existing blister-packaging lines. The launch highlighted the industry's move toward alternative blister materials that combine packaging functionality with improved end-of-life potential.
- Interactive Data Analysis Dashboard
- Company Analysis Dashboard for high growth potential opportunities
- Research Analyst Access for customization & queries
- Competitor Analysis with Interactive dashboard
- Latest News, Updates & Trend analysis
- Harness the Power of Benchmark Analysis for Comprehensive Competitor Tracking
Global High Barrier Packaging Films For Pharmaceuticals Market, Supply Chain Analysis and Ecosystem Framework
To support market growth and help clients navigate the impact of geopolitical shifts, DBMR has integrated in-depth supply chain analysis into its Global High Barrier Packaging Films For Pharmaceuticals Market research reports. This addition empowers clients to respond effectively to global changes affecting their industries. The supply chain analysis section includes detailed insights such as Global High Barrier Packaging Films For Pharmaceuticals Market consumption and production by country, price trend analysis, the impact of tariffs and geopolitical developments, and import and export trends by country and HSN code. It also highlights major suppliers with data on production capacity and company profiles, as well as key importers and exporters. In addition to research, DBMR offers specialized supply chain consulting services backed by over a decade of experience, providing solutions like supplier discovery, supplier risk assessment, price trend analysis, impact evaluation of inflation and trade route changes, and comprehensive market trend analysis.
Data collection and base year analysis are done using data collection modules with large sample sizes. The stage includes obtaining market information or related data through various sources and strategies. It includes examining and planning all the data acquired from the past in advance. It likewise envelops the examination of information inconsistencies seen across different information sources. The market data is analysed and estimated using market statistical and coherent models. Also, market share analysis and key trend analysis are the major success factors in the market report. To know more, please request an analyst call or drop down your inquiry.
The key research methodology used by DBMR research team is data triangulation which involves data mining, analysis of the impact of data variables on the market and primary (industry expert) validation. Data models include Vendor Positioning Grid, Market Time Line Analysis, Market Overview and Guide, Company Positioning Grid, Patent Analysis, Pricing Analysis, Company Market Share Analysis, Standards of Measurement, Global versus Regional and Vendor Share Analysis. To know more about the research methodology, drop in an inquiry to speak to our industry experts.
Data Bridge Market Research is a leader in advanced formative research. We take pride in servicing our existing and new customers with data and analysis that match and suits their goal. The report can be customized to include price trend analysis of target brands understanding the market for additional countries (ask for the list of countries), clinical trial results data, literature review, refurbished market and product base analysis. Market analysis of target competitors can be analyzed from technology-based analysis to market portfolio strategies. We can add as many competitors that you require data about in the format and data style you are looking for. Our team of analysts can also provide you data in crude raw excel files pivot tables (Fact book) or can assist you in creating presentations from the data sets available in the report.